HBR-1020R
Portable Hand-held Edge Rounding (Radius) Machine
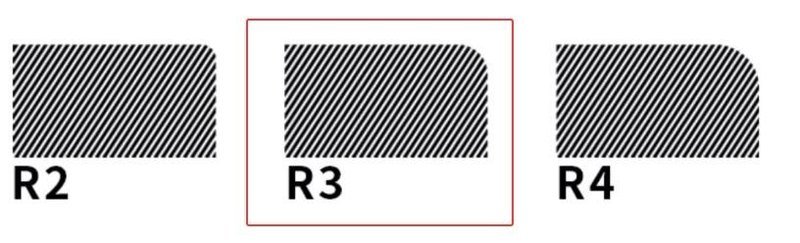
On a sharp edge the paint film thins, shrinks back and lifts; corrosion almost always starts there. Rounding the edge to R2–R5 lets the coating hold full thickness over the edge. On die sets a rounded edge also prevents scratching during assembly and cuts to the hands.
Machinery · Radius and Edge Preparation Machines
Portable Hand-held Edge Rounding (Radius) Machine
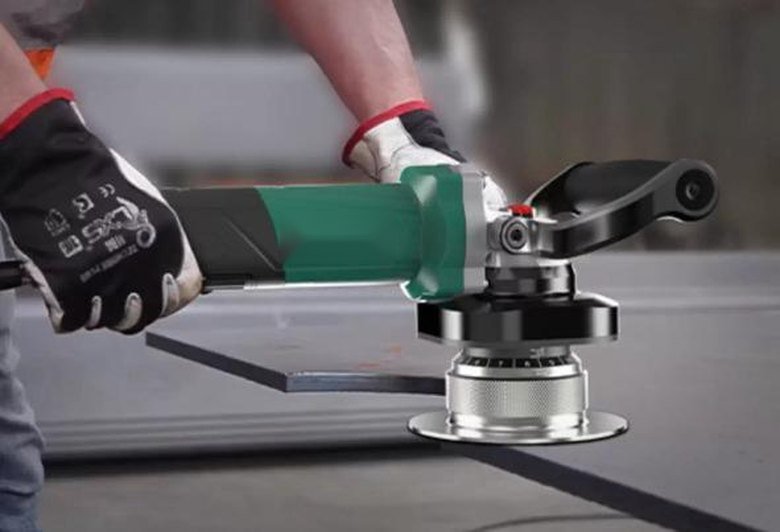
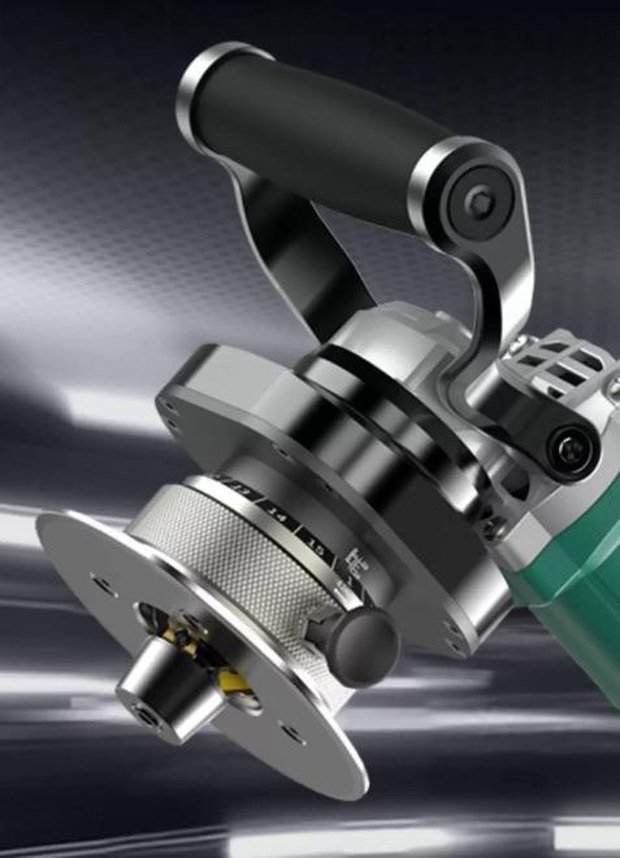
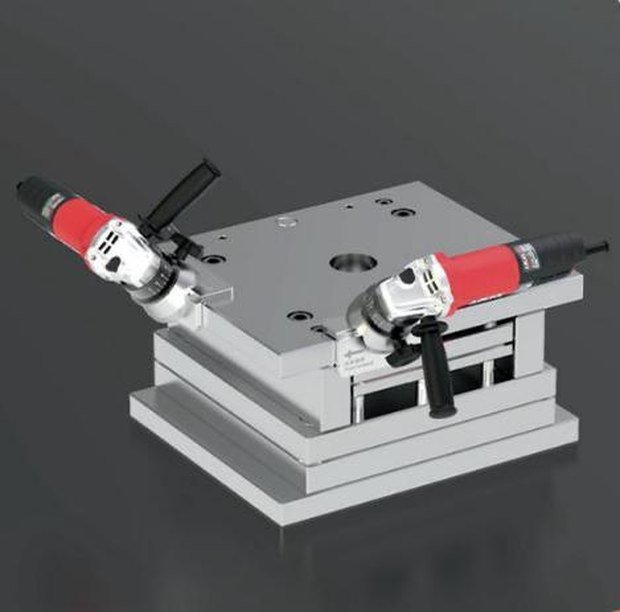
The HBR-1020R is a hand-held radius machine developed for mould base and die set manufacturing. It rounds the sharp edge of the workpiece to the required radius in a single pass with an indexable insert. Unlike hand grinding, the guide wheel follows the edge itself, the insert leaves a constant profile and the result does not change from operator to operator.
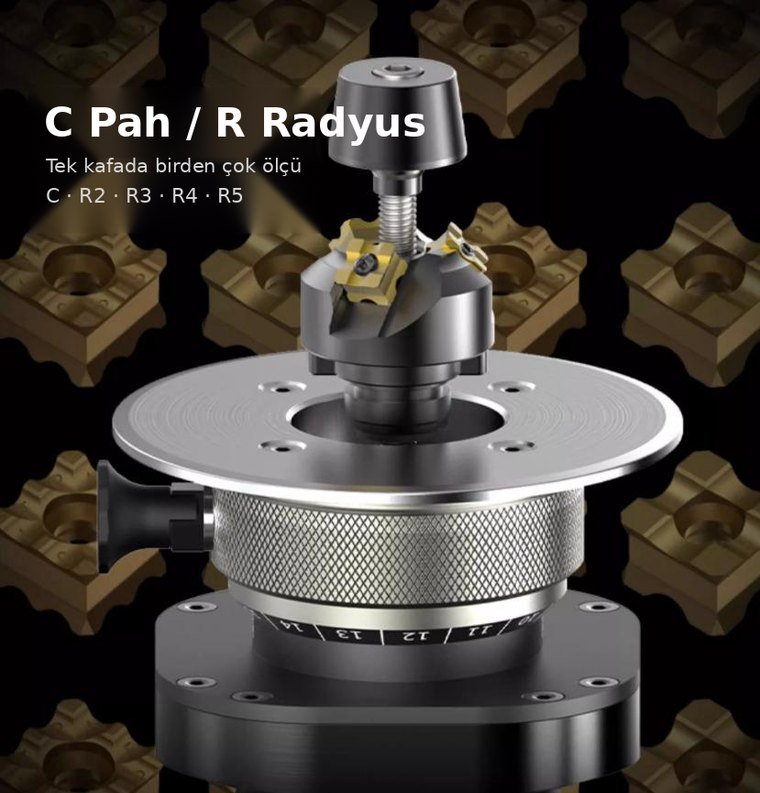
The radius size is selected by changing the head: R2, R3, R4, R5. A stepless precision thread adjustment fine-tunes the depth of cut within the same head; once set, no re-adjustment is needed in series work. A C-type head can also be fitted for chamfering, but the machine's real job is the radius.
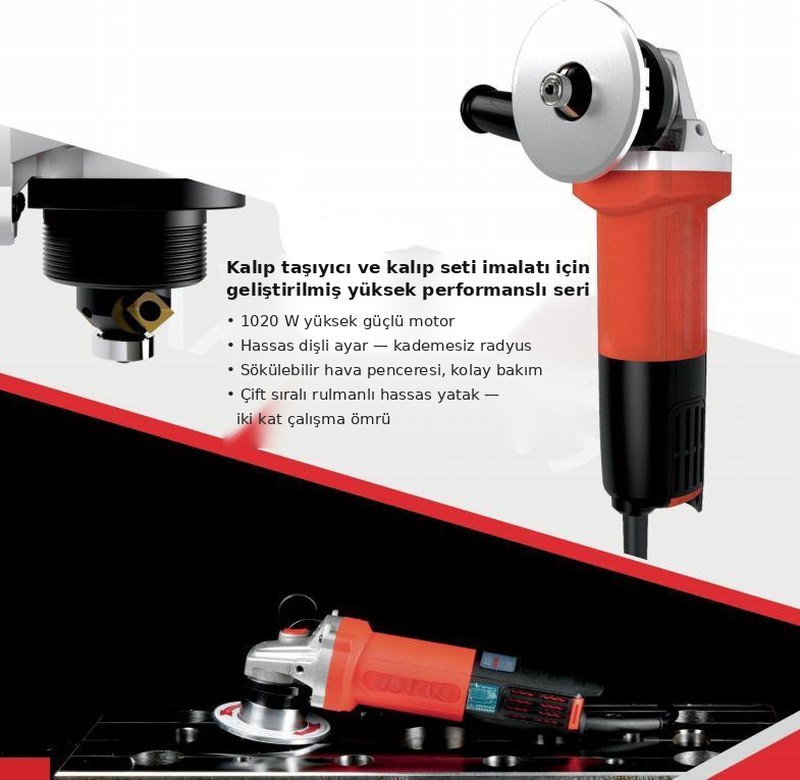
A 1020 W motor, precision bearing housing with double-row bearings and a detachable wind window make it suitable for continuous work. The inserts are indexable, so at end of life the insert is turned rather than the head replaced.
Technical data
| Rated power | 1020 W |
|---|---|
| Voltage | 230 V – 50 Hz |
| No-load speed | 11,000 rpm |
| Radius range | R1 – R4 mm (head options: R2 · R3 · R4 · R5) |
| Guide wheel | Ø19 mm (optional Ø7 mm) |
| Blind zone | 9.5 mm (with Ø19 mm wheel) |
| Plate thickness | 5 mm and above |
| Insert | Indexable HN865 cermet |
| Workable hardness | up to 48 HRC (unhardened steel) |
| Suitable materials | Steel, copper, aluminium, carbon fibre board |
| Adjustment | Precision thread — stepless |
| Bearings | Precision housing with double-row bearings |
| Weight | 2.7 kg |
| Brand | HBTAKIM |
Inserts
| Insert | Radius | Cutting material | Size (mm) | Hole | Suitable material |
|---|---|---|---|---|---|
| R2 | R2 mm | HN865 cermet | 9.5 × 9.5 × 4.0 | Ø4.3 mm | Unhardened steel, < 48 HRC |
| R3 | R3 mm | HN865 cermet | 9.5 × 9.5 × 3.2 | Ø4.3 mm | Unhardened steel, < 48 HRC |
| R4 | R4 mm | HN865 cermet | 9.5 × 9.5 × 3.2 | Ø4.3 mm | Unhardened steel, < 48 HRC |
| R5 | R5 mm | HN865 cermet | 9.5 × 9.5 × 3.2 | Ø4.3 mm | Unhardened steel, < 48 HRC |
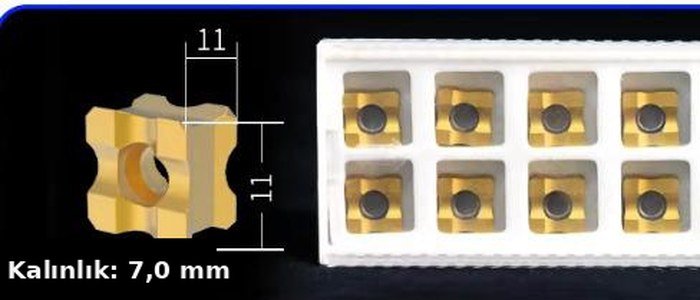
| Large head insert | R2 – R5 mm | Coated carbide | 11 × 11 × 7.0 | Centre hole | Steel, cast iron, aluminium |
Applications
- Radius on mould base and die set edges
- Edge rounding before painting (ISO 8501-3)
- Rounding hole mouths and flange edges
- Removing sharp edges after laser / plasma cutting
- Edge preparation on structural steel and sections
- Edge breaking on aluminium and copper parts
Scope of supply
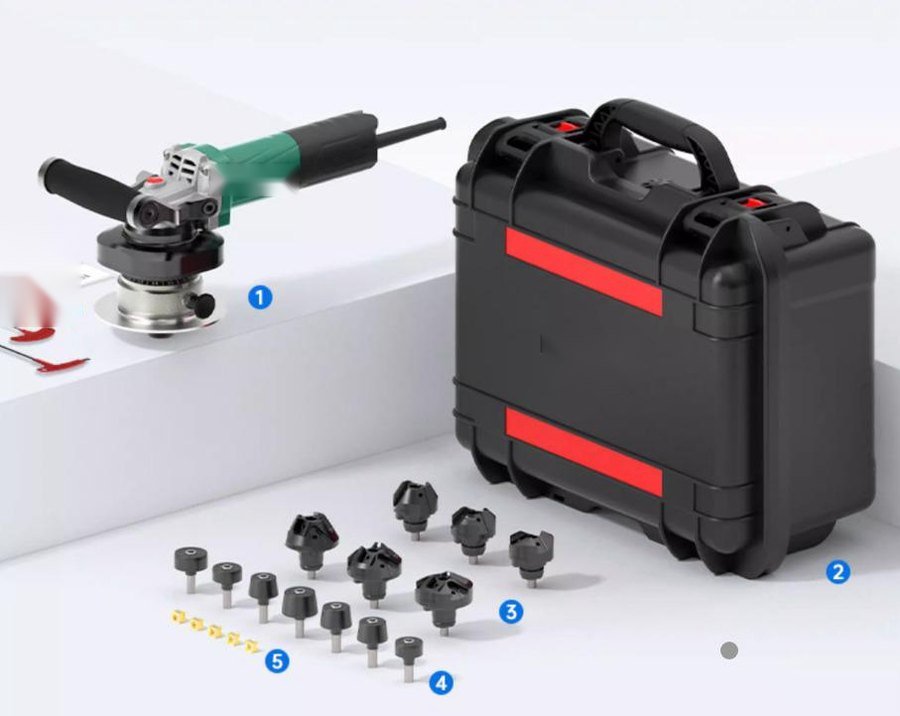
- 1 — HBR-1020R machine body
- 2 — Impact-resistant carrying case
- 3 — Radius cutter heads (R2 / R3 / R4 / R5)
- 4 — Guide wheel set
- 5 — Spare cermet inserts and clamping screws
- 6 — Hex key set, spare carbon brushes, side handle
Guide wheel and blind zone
Because the guide wheel rides on the edge, an area equal to the wheel radius cannot be machined. With a Ø19 mm wheel the blind zone is 9.5 mm in both directions. On outside corners the corner can be rounded if the workpiece radius is larger than the wheel radius; on inside corners the outward radius is a blind spot. A Ø7 mm guide wheel reduces the blind zone to 3.5 mm.
Specifications are subject to change without notice.
Gallery
Machine, head and kit.