
Carbide Burrs
Tungsten Carbide Rotary Burrs · Shape Series A – N
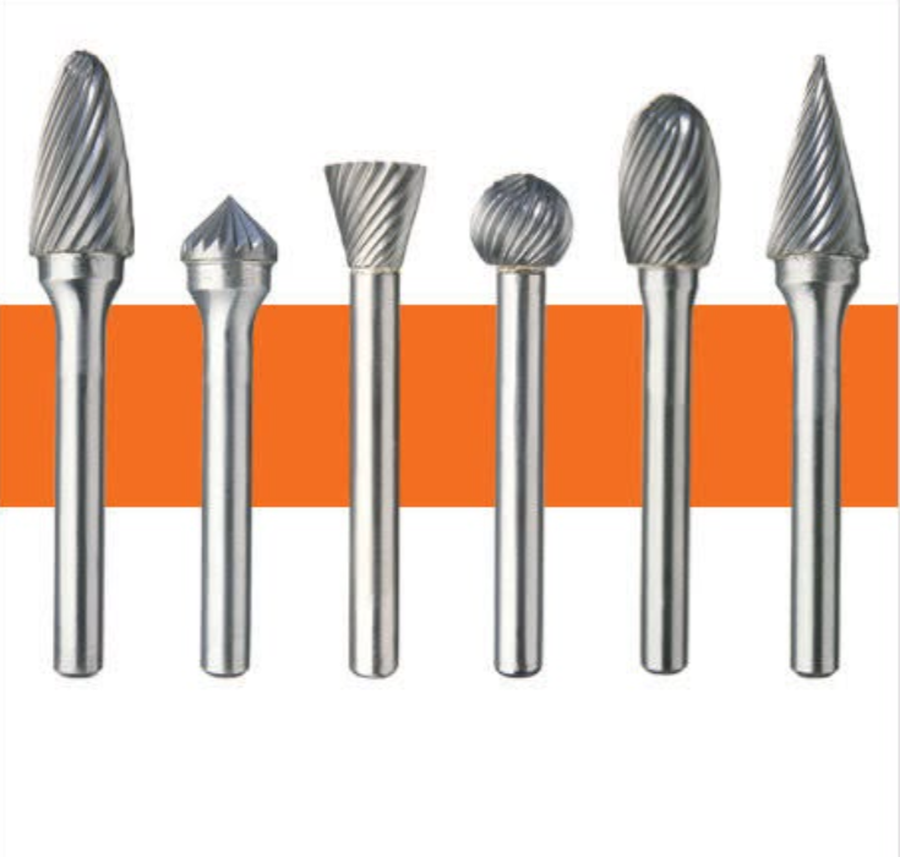
Use double cut in steel, stainless and cast iron; use single cut or the aluminium geometry in aluminium, copper, brass and plastics. The wrong tooth style loads the tool and burns the surface.
Machinery · Deburring, Finishing and Die Tools
Tungsten Carbide Rotary Burrs · Shape Series A – N
A carbide burr is a small rotary cutter used in pneumatic or electric die grinders. Unlike an abrasive point it does not grind the material away, it removes real chips: the workpiece stays cooler, the surface does not burn and the tool does not load up. It is the standard hand tool for everything from weld dressing to die repair.
The cutting head is made from sintered tungsten carbide (WC-Co) and brazed to — or machined in one piece with — the shank. It works on material up to 65 HRC, lasts 20–40 times longer than an abrasive point and produces chips rather than dust, which keeps the work area cleaner.
Tooth style is chosen by material. Double cut (cross cut) gives short chips in steel, stainless and cast iron and is the most common. Single cut is used in aluminium, copper and plastics; it throws a long chip and prevents wrapping. The aluminium cut geometry stops loading in soft metals.
Technical data
| Cutting material | Sintered tungsten carbide (WC-Co) |
|---|---|
| Head diameter | Ø3 – 16 mm |
| Shank diameter | 3 mm / 6 mm (special: 1/8" · 1/4") |
| Shank length | 38 / 50 / 100 / 150 mm |
| Shape series | A · B · C · D · E · F · G · H · J · K · L · M · N |
| Tooth style | Double cut · Single cut · Aluminium cut |
| Coating | Uncoated / TiAlN (optional) |
| Material hardness | up to 65 HRC |
| Speed | Ø3 mm: 45,000 rpm — Ø16 mm: 15,000 rpm |
| Brand | HBTAKIM |
Applications
- Weld dressing and excess metal removal
- Deburring and gate cleaning on castings
- Die repair and form correction
- Edge cleaning after laser / plasma cutting
- Hole chamfering and edge breaking
- Surface dressing in stainless and aluminium
Sets and packaging
- Set of 5 — A, C, D, F, G · Ø6 mm shank
- Set of 6 — Ø6 mm shank, double cut (plastic case)
- Set of 10 — mixed shapes, wooden/metal case
- Workshop set of 20 — mixed double + single cut
- Single item — any shape and size
- Extension shank 100 / 150 mm for deep forms
Specifications are subject to change without notice.